Table of Contents
A gull-wing lead can look straight from above and still sit too far above the seating plane to form the intended solder joint. QFP lead coplanarity inspection therefore has to distinguish lateral lead alignment from out-of-plane displacement.
The inspection objective is a measurable package-geometry decision before assembly. It is separate from electrical testing, authenticity assessment and post-reflow solder-joint inspection. A clear microscope image alone does not answer every one of those questions.
What does lead coplanarity measure?
Lead coplanarity describes the relationship between the package’s lead contact surfaces and its defined seating plane. The applicable package drawing and measurement convention determine the datum and limit; the molded body is not automatically the reference surface.
NXP’s archived PFP package application note, AN1580, gives a useful manufacturer example of how a seating plane and lead contact surfaces are defined. Its specific package dimensions and tolerance are not universal QFP acceptance limits. For the purchased QFP, obtain the drawing for the exact package code and revision from the component manufacturer.
Record pitch, lead dimensions, stand-off and coplanarity separately. A package can meet one characteristic and fail another. Measuring body height, for example, cannot substitute for measuring how the lead feet relate to the specified plane.
How should an incoming inspection measure the leads?
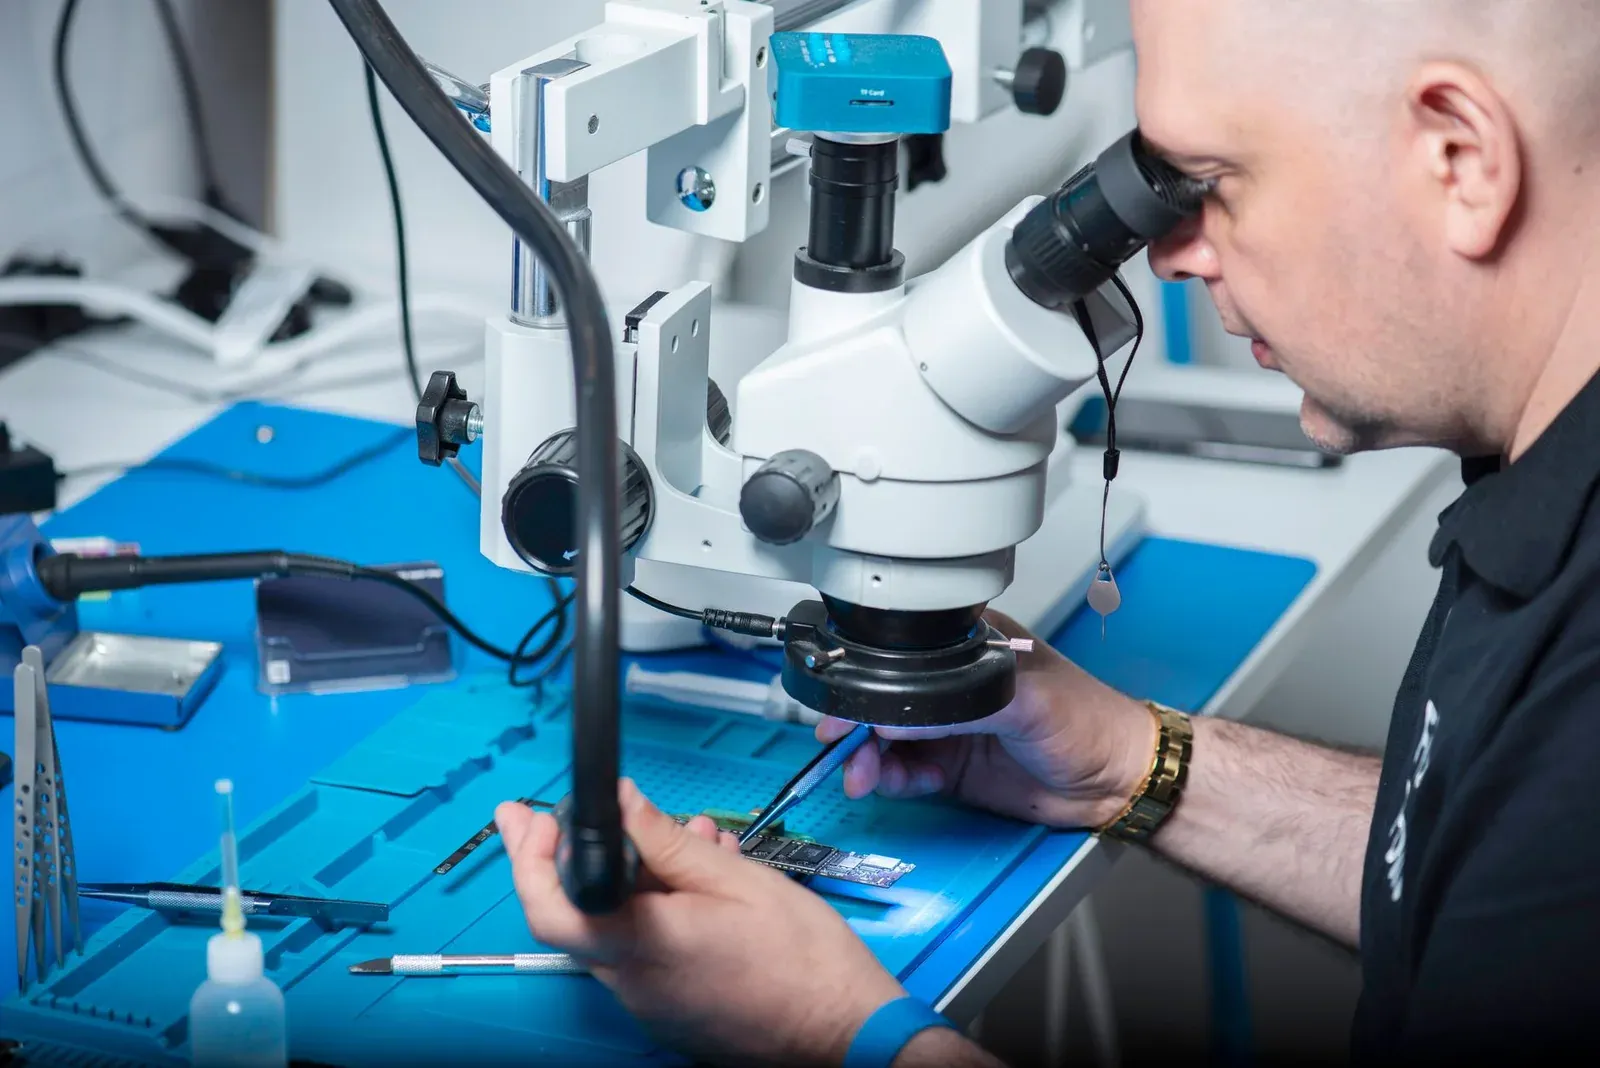
Use a method capable of resolving the specified three-dimensional geometry without deforming the leads. Define the support, orientation, datum construction and measurement uncertainty before using the result for acceptance.
A top-down optical image is useful for bent IC leads, spacing and obvious damage, but generally does not establish out-of-plane displacement. Depending on the required tolerance and available equipment, inspection may need a calibrated side-view method, optical metrology or an appropriate three-dimensional measurement system.
The inspection record should identify:
- Manufacturer part number, package drawing and revision.
- Lot identity, packing format and the sample-selection method.
- Fixture and support arrangement, including how force on the leads is avoided.
- Datum construction, instrument settings, resolution and calibration status.
- Measured characteristic, result, uncertainty and the agreed decision rule.
Do not press the package flat to improve the reading. That can alter the characteristic being measured. Similarly, a lead that has already been straightened is no longer evidence of the as-received condition.
A borderline result needs a decision rule
A result close to the limit must be interpreted using the agreed measurement decision rule, not simply rounded until it appears acceptable. Instrument display resolution and measurement uncertainty are different quantities.
Take a drawing limit of 0.10 mm, a measured result of 0.09 mm and an expanded uncertainty of 0.02 mm. Under a conservative rule that accepts only when result + uncertainty ≤ limit, this measurement would not qualify for acceptance because 0.09 + 0.02 = 0.11 mm. It also does not, by itself, prove that the true value exceeds the drawing limit.
The practical response is the one defined in the purchasing and inspection procedure: improve the measurement, obtain a capable independent assessment, or hold the material pending disposition.
The measurement-uncertainty procurement guide explains how to agree those decision rules when buying an external inspection service. Include the rule in the work order before results arrive.
What should happen when bent or lifted leads are found?
Preserve the as-received evidence, contain the affected material and determine whether the damage pattern points to the package, carrier or handling process. Do not immediately rework the leads and then report that the incoming lot passed.
| Observed pattern | Useful follow-up | Disposition boundary |
|---|---|---|
| Damage concentrated at one tray edge | Compare tray pockets, stacking and shipping condition | Check adjacent pockets and affected carrier locations |
| Repeated lead deformation in the same package position | Review orientation and handling contact points | Investigate systematic handling before expanding screening |
| Mixed damage with missing lot separation | Reconstruct lot and packing identity | Hold uncertain populations apart from accepted material |
| Geometry passes but assembly joints fail | Review land pattern, paste, placement and reflow evidence | Do not attribute all assembly defects to coplanarity |
Link the escalation to the established incoming sampling plan. A photograph of one damaged device does not define the extent of the lot problem, while a few acceptable samples do not erase evidence of a recurring packaging defect.
Can a formed or repaired lead be released as an ordinary replacement?
Only through an explicitly authorized process with appropriate post-rework acceptance and traceability. Mechanical restoration may introduce additional concerns, including finish damage or lead stress, that are not resolved by a better-looking outline.
For a component replacement assessment, distinguish an alternate manufacturer part from a reworked lot of the original part. They need different evidence and approval routes. A substitute with a different package drawing must be assessed against its own dimensions and the board’s assembly requirements.
The inspection deliverable should be a lot-level geometry report linked to the original images and carrier locations, with clear accepted, held and rejected quantities. That gives procurement a basis for supplier disposition and gives manufacturing a defined population to release.
Frequently Asked Questions (FAQ)
Does electrical testing establish lead coplanarity?
No. Electrical tests and lead-geometry measurements answer different questions. A functioning device can still have leads outside the package's mechanical acceptance limits.
Can the molded package body be used as the seating datum?
Only if the applicable drawing and measurement method define it that way. Gull-wing lead coplanarity commonly references lead contact surfaces and a specified seating plane.
Does one bent lead prove a counterfeit part?
No. Bent leads may result from packaging, transport, handling or other causes. Preserve the evidence and investigate the damage without treating it as a standalone authenticity conclusion.